Scaling a product from a single prototype to 100,000 units is one of the biggest tests a hardware team will face, and reliable custom CNC machining gives that journey a practical, repeatable path. The reason is simple: the same digital design that produces the first test part can guide every part that follows, so a team can check fit, function, and finish early, then grow volume without redesigning the product from scratch. When the process is planned well, the move from prototype to 100k units becomes a series of controlled steps rather than one risky leap.
This guide explains how to scale from prototype to 100k units with reliable custom cnc machining, what changes at each stage, and which decisions protect quality, cost, and delivery as orders grow. It is written for product teams, founders, and buyers who need a clear picture of the process before they commit to larger production runs.
Key Takeaways: Scale in stages, prototype, pilot, low volume, then high volume, rather than jumping straight to 100,000 units. Review the design for manufacturability before volume grows, because features that work for one part can slow down or vary across thousands. Choose the material and machining process for the production environment, not only for the prototype. Measure real parts at every stage, since tool wear, heat, workholding, and material variation can shift dimensions over long runs. Keep costs, finishes, and lead times in balance by quoting at several quantities and freezing specifications before full production.
What is scale from prototype to 100k units with reliable custom cnc machining? It is the process of taking a validated prototype design and producing it in growing, controlled batches using computer numerical control machining, until the operation can consistently deliver 100,000 units or more to the same specification. CNC machining, often shortened to CNC, uses computer controlled tools to cut, mill, turn, and shape material with repeatable precision, which makes it well suited to both one off prototypes and large production orders.
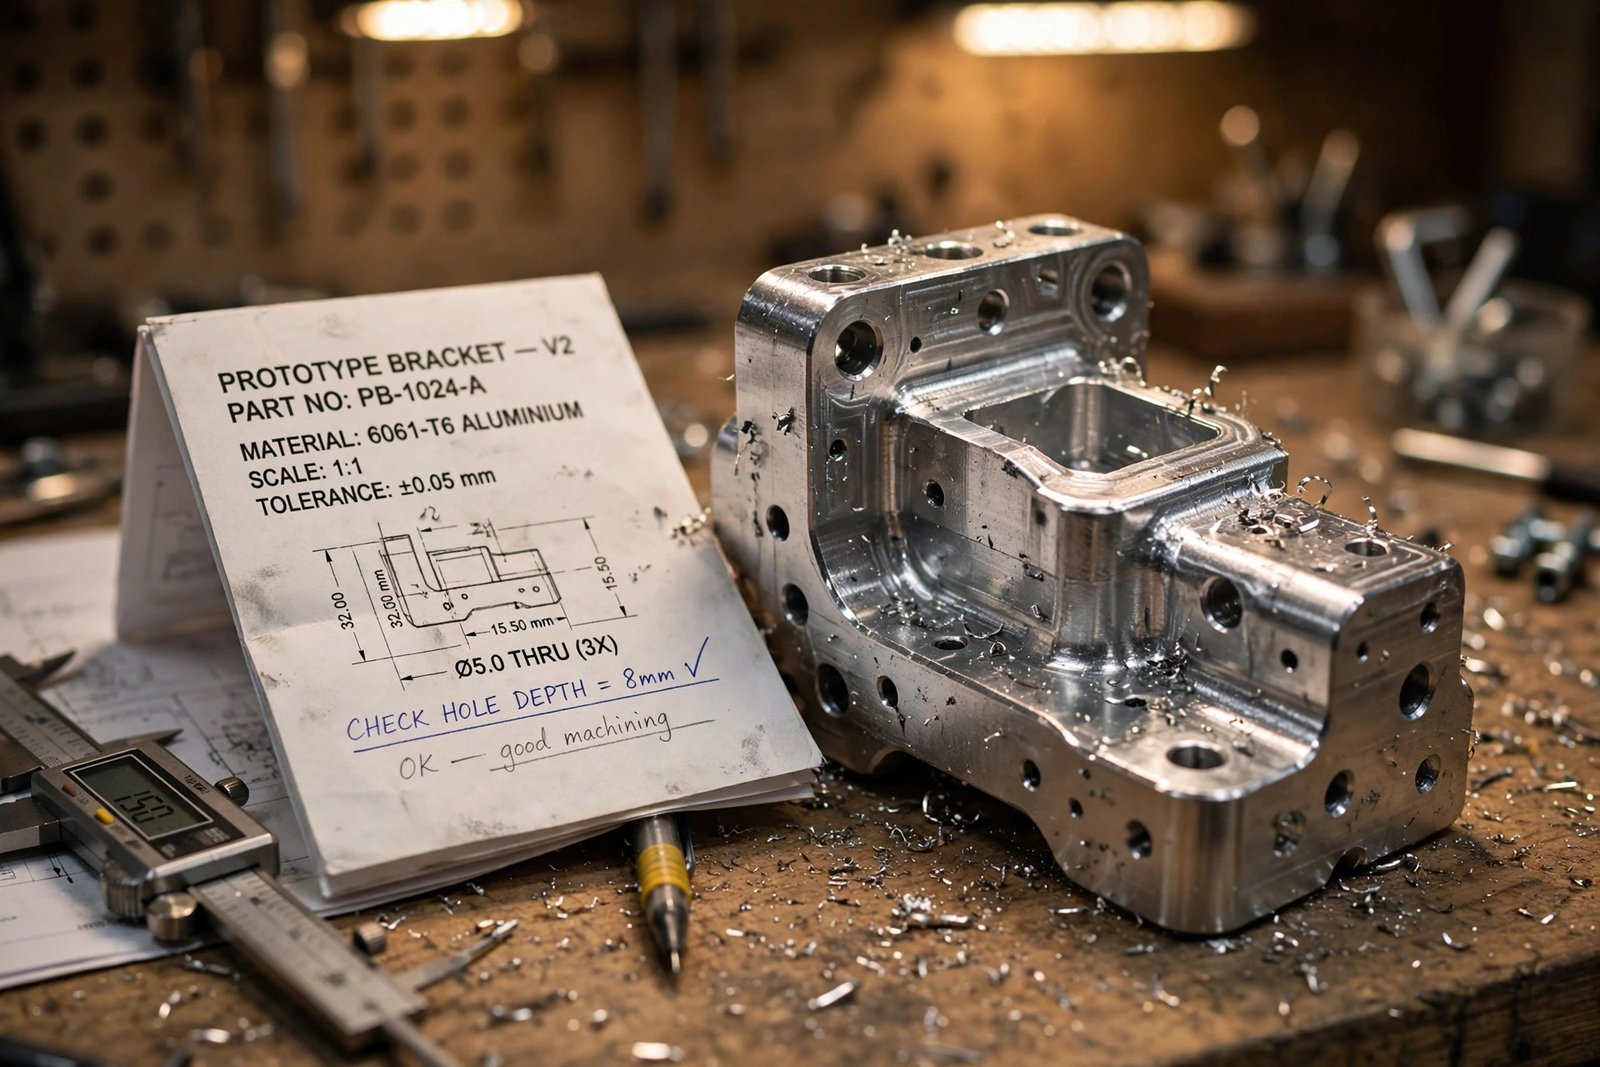
The benefits of this approach are practical rather than theoretical. A prototype can be made directly from a CAD model, which is the digital drawing of the part, without the cost and delay of dedicated production tooling. That lets engineers test real geometry, interfaces, fasteners, and surface quality in the actual material, and it gives the whole team a physical baseline for what production parts should look and feel like.
The scale from prototype to 100k units with reliable custom cnc machining benefits also include continuity. Because prototype and production parts can come from the same design data, lessons learned during testing carry forward into tooling choices, inspection plans, and finishing steps. A supplier that handles both stages can keep that knowledge in one place, which reduces handover errors and repeated explanations.
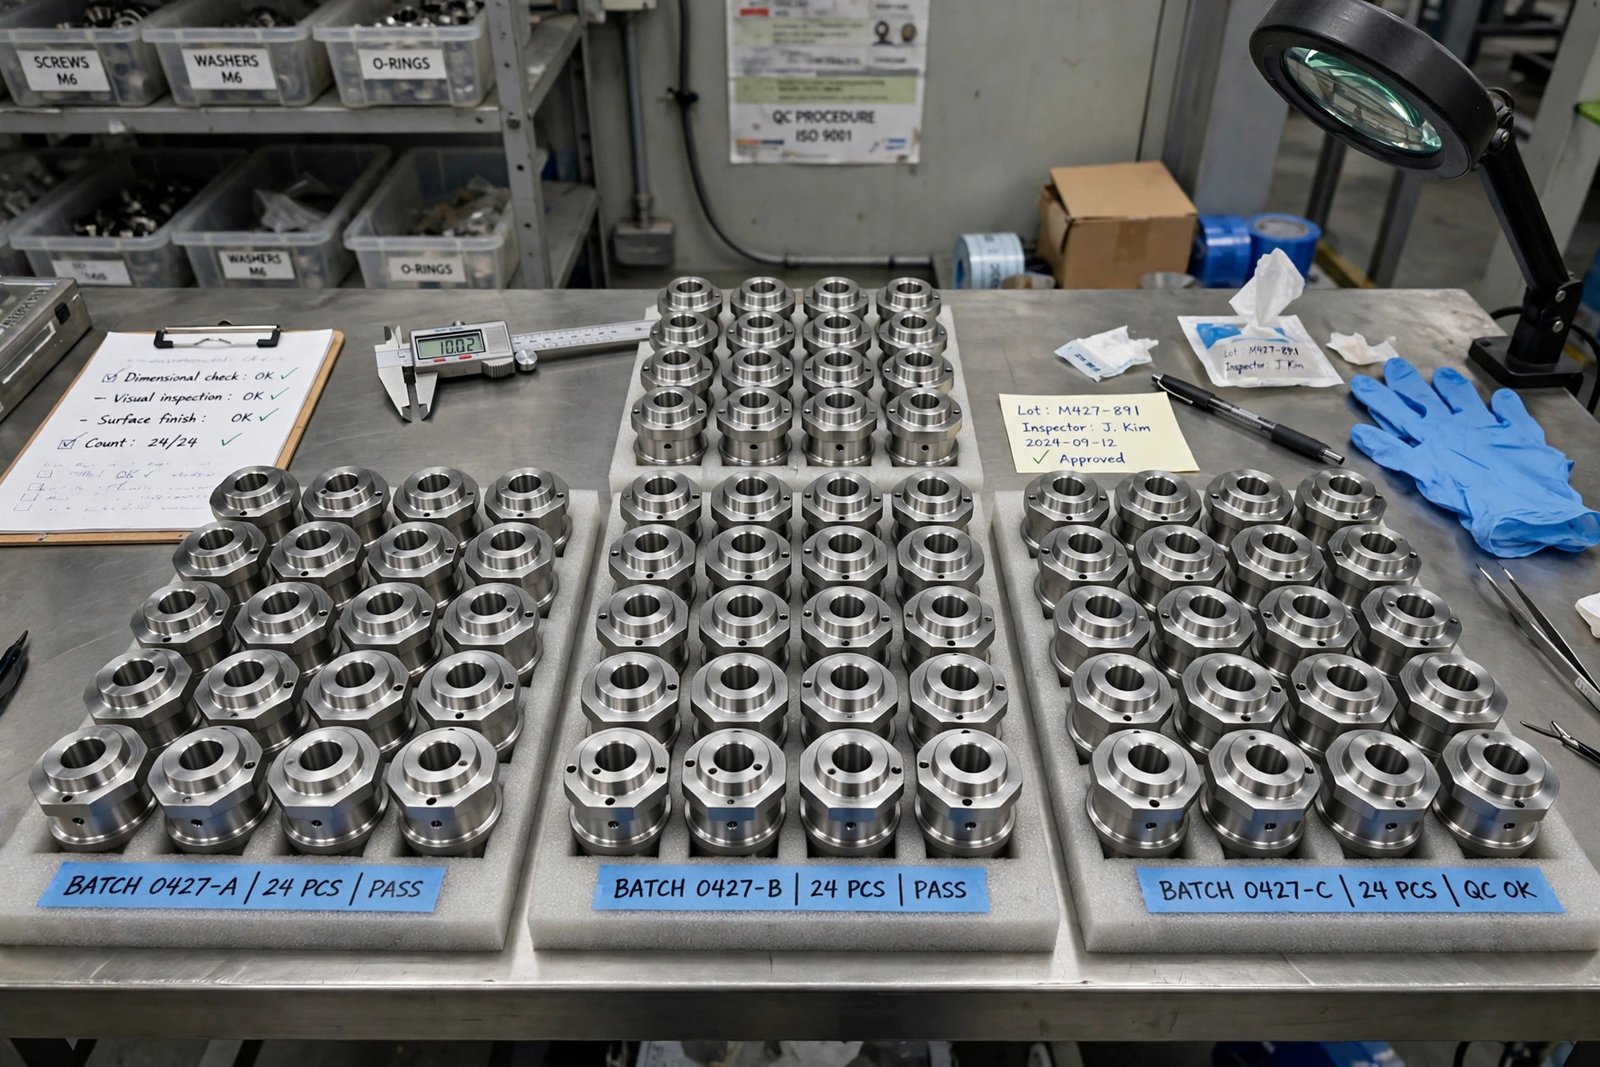
Still, scaling is not only about making more parts faster. Each stage introduces new risks, from material supply and machine capacity to inspection workload and packaging, and each risk is easier to manage when it is found at a small batch size. That is why experienced manufacturers insist on acceptance criteria at every step, so production only advances when dimensional results, material requirements, and process performance meet the agreed specification.
Another early decision is whether the design is truly ready for volume. A part that works beautifully as a prototype may carry deep pockets, very thin walls, sharp internal corners, or tolerances tighter than the function requires. In small numbers those features are manageable, but across thousands of parts they add machining time, tool changes, and variation. A design for manufacturability review, usually called a DFM review, looks for exactly these issues before production begins.
In a DFM review, engineers check tool access, workholding, material behaviour, and the number of setups needed to machine the part. They may suggest consistent feature placement, practical internal radii, standard drill sizes, and looser tolerances on noncritical dimensions while keeping tight control where function demands it. Those changes protect performance while removing avoidable cost, and they are far cheaper to make before a large order is placed.
Why does a CNC prototype matter before mass production?
A CNC prototype matters because it turns an idea on screen into a testable object. Engineers can check whether parts fit together, whether fasteners sit correctly, whether moving parts clear each other, and whether the surface finish suits the application. Testing in the real production material is especially valuable, since a plastic mockup or a different alloy may hide strength, weight, or corrosion problems that only appear later.
For a useful prototype, the team should agree in advance what the part must prove. Is it geometry and fit, mechanical performance, surface quality, or all three? Clear test goals keep the prototype honest and prevent a good looking sample from being mistaken for a production ready design.
How should a design be prepared for repeatable manufacturing?
A design should be prepared by reviewing it specifically for volume production, not only for function. That means checking wall thickness, pocket depth, corner radii, hole sizes, and tolerance demands against what machining can repeat reliably. Features should be consistent where possible, so the same setup and tooling can serve many parts without constant adjustment.
What to check in a DFM review
- Tool access: can the cutting tool reach every feature without unusual setups or custom tooling?
- Workholding: can the part be held firmly and repeatedly in the same position for every batch?
- Material behaviour: will the chosen material machine cleanly, hold its shape, and suit the operating environment?
- Tolerances: are tight tolerances reserved for dimensions that truly affect fit or function?
- Standard sizes: can standard drills, taps, and radii replace custom features without harming performance?
Which materials and processes suit production at scale?
Material choice affects workability, strength, weight, corrosion resistance, and cost, so it should match the final use of the part. Aluminium 6061-T6 is widely used for lightweight housings and brackets, while stainless steel 316L is a common choice where corrosion resistance matters. Engineering plastics such as POM, nylon, and PEEK offer different combinations of stiffness, friction, chemical resistance, and temperature resistance, and each machines differently.
The machining process should match the shape and volume of the part. Three axis milling handles many simpler parts, while four and five axis milling can reach multiple surfaces with fewer setups, which can improve consistency on complex geometry. CNC turning suits shafts, pins, and bushings, and wire EDM can create complex features in conductive materials. Choosing among them means weighing material specifications, functional requirements, production volume, and finishing needs together.
How does production scale through structured batches?
Production scales best through structured batches, with each stage proving something before the next one begins. Skipping from one prototype to a 100,000 unit order can hide process problems until they are expensive to fix, while small batches reveal defect patterns, cycle time problems, and inspection gaps while changes are still cheap.
| Stage | What it proves | Typical volume |
|---|---|---|
| Prototype validation | Geometry, fit, material suitability, and functional requirements | One part or a small number of parts |
| Pilot production | Cycle times, repeatability, inspection procedures, and finishing operations | A controlled pilot batch |
| Low volume manufacturing | Quality trends, process stability, and production planning | Approximately 100 to 1,000 units |
| High volume production | Consistent delivery at scale using validated processes and planned capacity | Toward 100,000 units or more |
How is quality kept consistent across large orders?
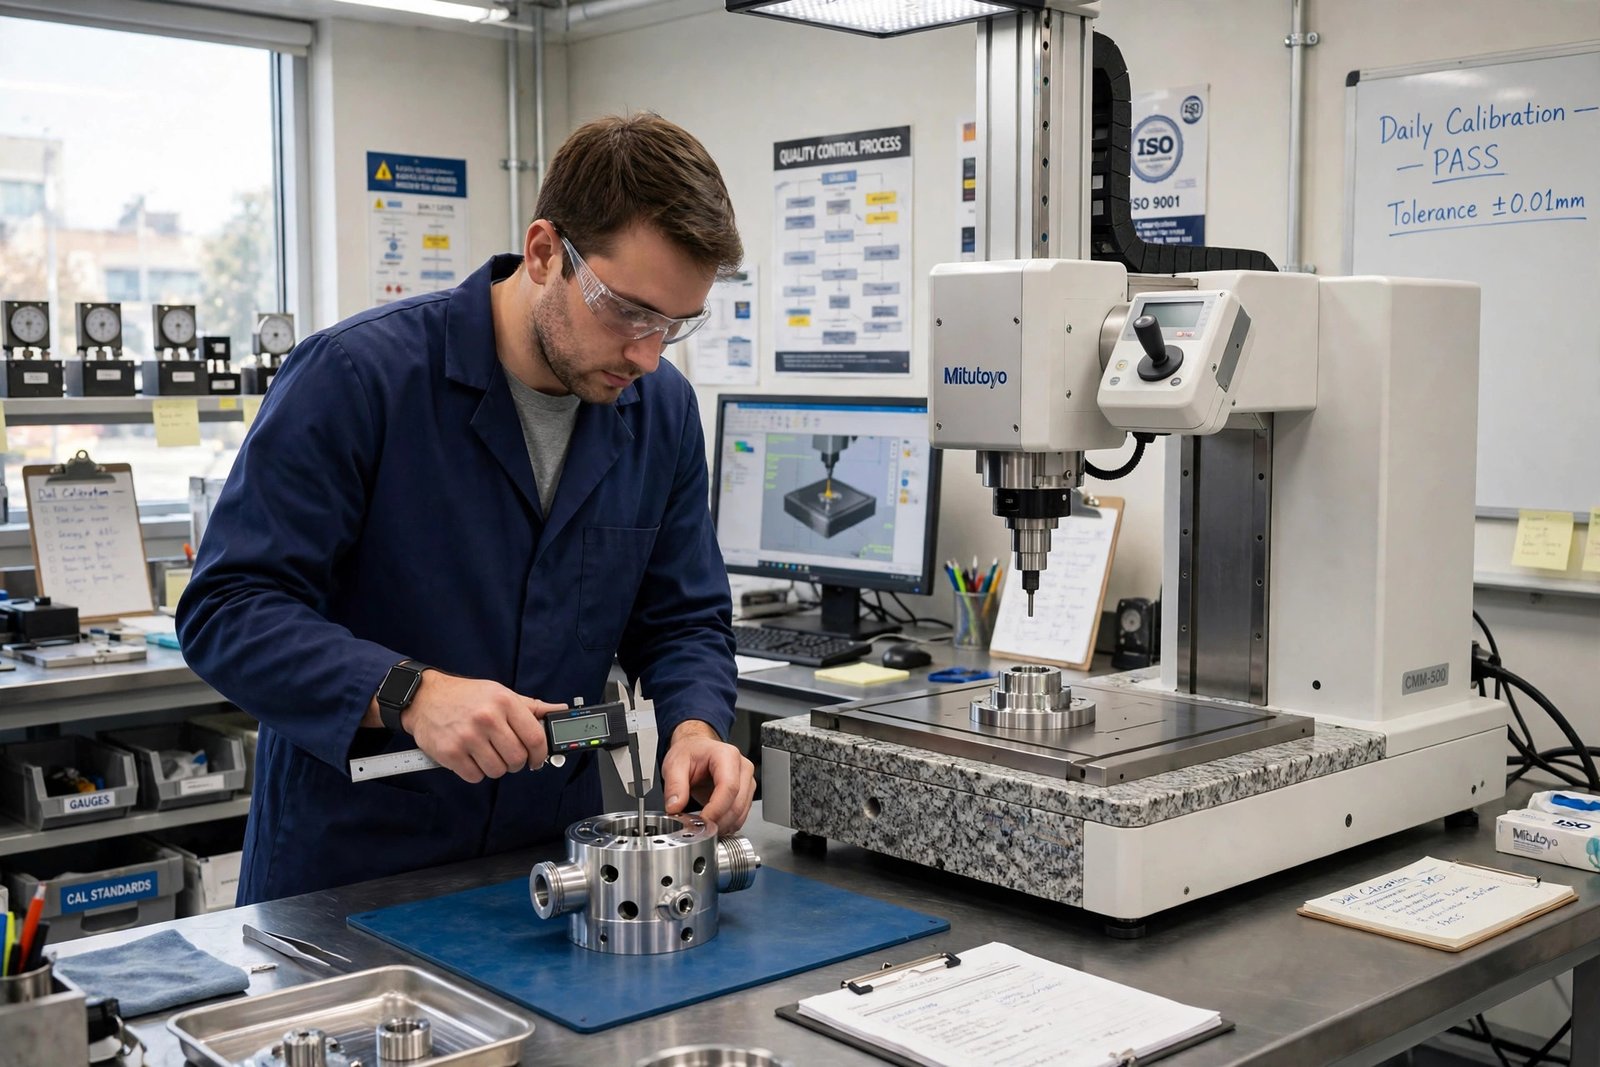
Quality is kept consistent by measuring real parts, not by assuming every part matches the digital model. Over long runs, tool wear, thermal change, workholding condition, and material variation can all shift dimensions, so scheduled inspections catch drift before it spreads across a large quantity.
A documented quality system supports that discipline. ISO 9001:2015, the widely used quality management standard, provides a framework for documented procedures, inspection records, and traceability. Depending on the component, manufacturers may use coordinate measuring machines, known as CMMs, precision gauges, and material analysis equipment to check requirements.
First article inspection is especially useful when ramping up, because it gives a full check of the first production parts against the drawing before the run continues. In process checks then keep production consistent, and inspection reports and material certificates provide documented evidence when a project requires it.
How do costs, finishes, and lead times balance at scale?
Unit cost depends on material, machining time, setup, tolerances, finishing, and quantity. Larger orders can spread programming and setup costs across more parts, but geometry and inspection requirements still shape the final price, so quoting at several quantities helps a buyer find a workable production approach. A quote for one quantity alone can hide the point where a different process or batch size becomes more efficient.
Surface finishes should match the component environment. Aluminium can be anodised to improve surface characteristics, powder coated for a decorative protective finish, and electroless nickel plated for specific wear and corrosion needs. Each added operation affects scheduling and cost, so finishes should be chosen for function and durability, not added by habit.
What should a buyer coordinate besides machine time?
A buyer should coordinate raw material procurement, tooling, machine availability, inspection capacity, packing, and transport against the delivery schedule. Large orders need more than free machine hours, and a delay in any one of those areas can stall the whole run. Clear communication about revisions and acceptance criteria protects the schedule, because it keeps outdated specifications out of production.
What mistakes slow down scaling most often?
The most common mistake is freezing a prototype design too early and treating it as production ready without a DFM review. Another is over specifying tolerances, which adds cost and inspection burden without improving function. A third is weak version control, where different teams work from different drawing revisions and produce parts to different standards.
- Freeze specifications and revision numbers before production.
- Reserve tight tolerances for dimensions that affect fit or function.
- Run a pilot batch and act on its findings before scaling.
- Confirm material supply, finishing capacity, and inspection time in the schedule.
- Keep inspection records so trends are visible across batches.
For readers following manufacturing and business stories, The Weird News Blog covers a wide mix of business topics alongside its other reporting, and this guide fits that practical, explanatory approach: clear steps, real trade offs, and no promises that a complex production ramp will be effortless.
Frequently Asked Questions
What is scale from prototype to 100k units with reliable custom cnc machining?
It is the staged process of moving a validated prototype design into growing CNC machined batches, using the same digital design data, until production can consistently deliver 100,000 units or more to specification.
Can the same supplier handle both prototypes and 100,000 units?
Yes, in many cases, but the buyer should verify it. Ask about machine capacity, material supply, inspection capability, and experience with both small and large batches, and confirm that prototype and production work follow one documented process.
Why not jump straight from a prototype to 100,000 units?
Jumping straight to full volume hides process problems until they are expensive. Pilot and low volume batches reveal defect patterns, cycle time issues, and inspection gaps while changes are still cheap and contained.
What is a DFM review and why does it matter?
A design for manufacturability review checks tool access, workholding, material behaviour, setups, and tolerances before production. It finds features that slow machining or cause variation, and suggests changes that protect performance while reducing avoidable cost.
How is quality checked during a large production run?
Quality is checked through documented procedures, first article inspection, in process checks, and scheduled inspections using tools such as CMMs and precision gauges where appropriate. Inspection records and material certificates provide evidence that parts met the specification.
What affects CNC machining lead time at scale?
Lead time is affected by part complexity, material availability, quantity, finishing operations, inspection requirements, and shipping arrangements. Simple parts may be fast, but complex or high volume orders need a schedule built around all of those factors.